Oil & Gas
Chemical and solvent applications supporting industrial processing and manufacturing requirements.
Industrial ProcessingSHK Chemtech Industries LLP serves diverse industrial sectors with high-quality chemical products supported by manufacturing expertise, process innovation and a sustainability-led approach.
Explore the industries supported by our products and manufacturing capabilities.
Chemical and solvent applications supporting industrial processing and manufacturing requirements.
Industrial Processing
Chemical and solvent products for relevant pharmaceutical manufacturing applications.
Pharma Manufacturing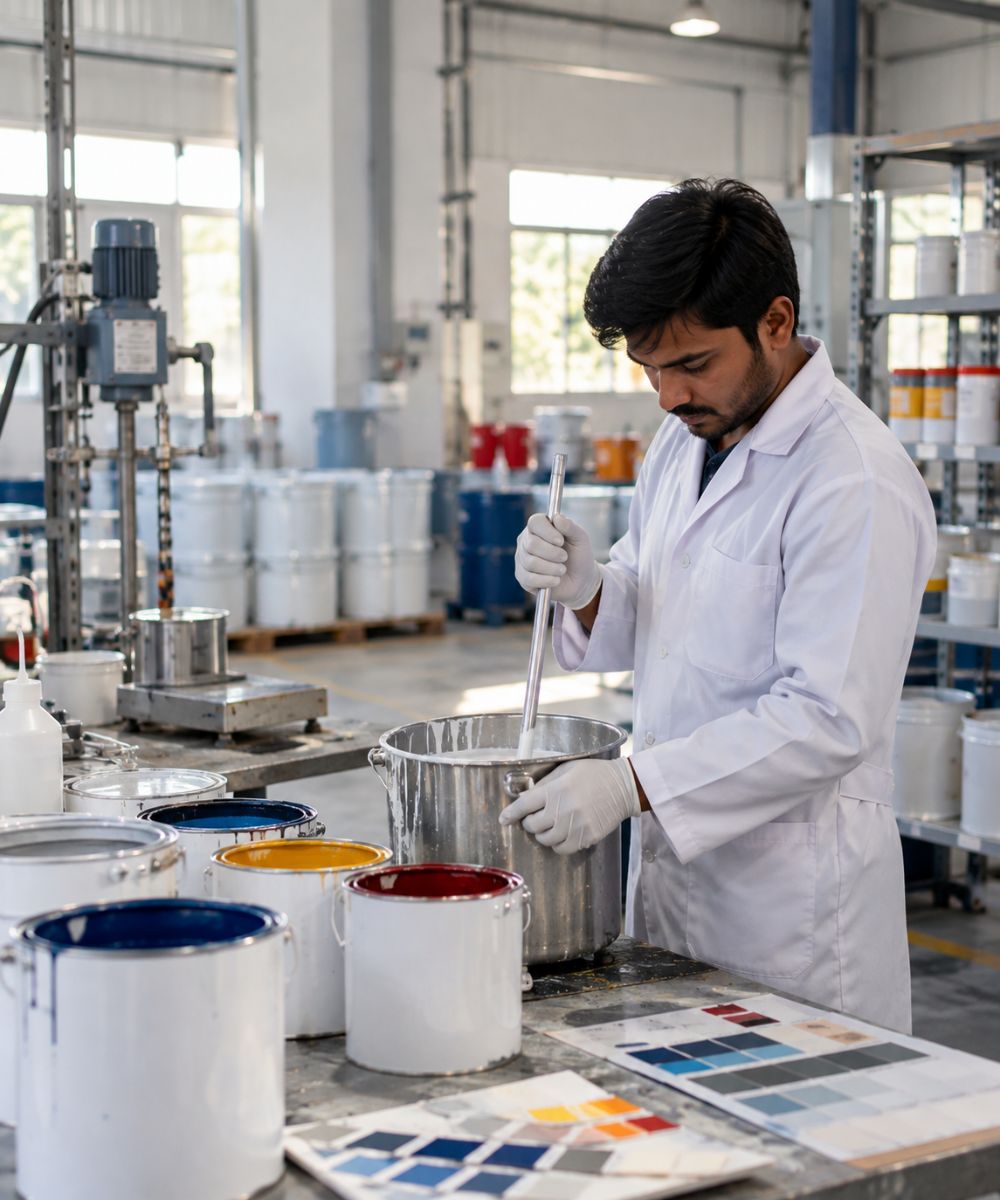
Solvent and chemical applications for coating formulations and related industrial processes.
Coating Applications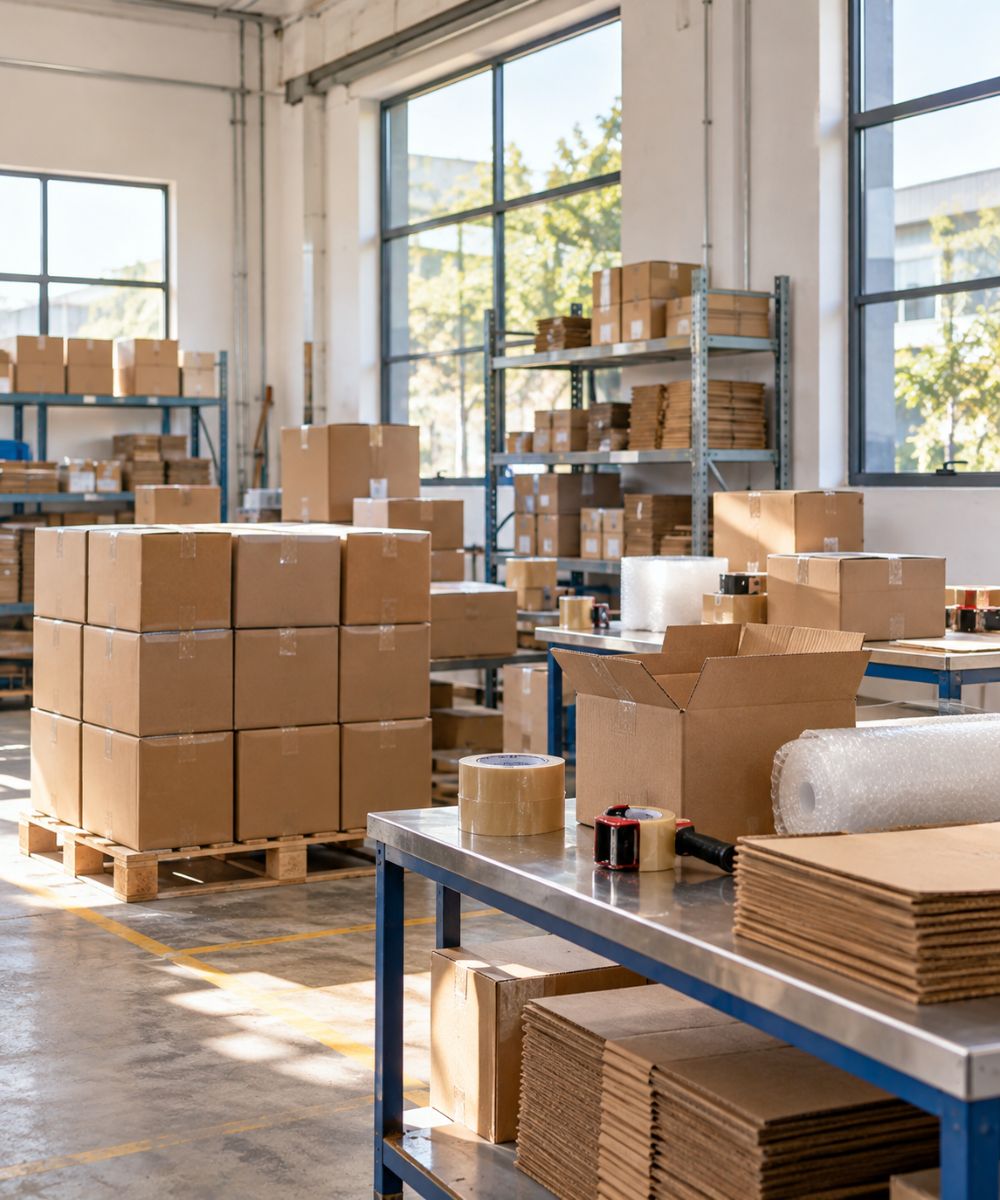
Chemical inputs for packaging materials and associated production processes.
Packaging Applications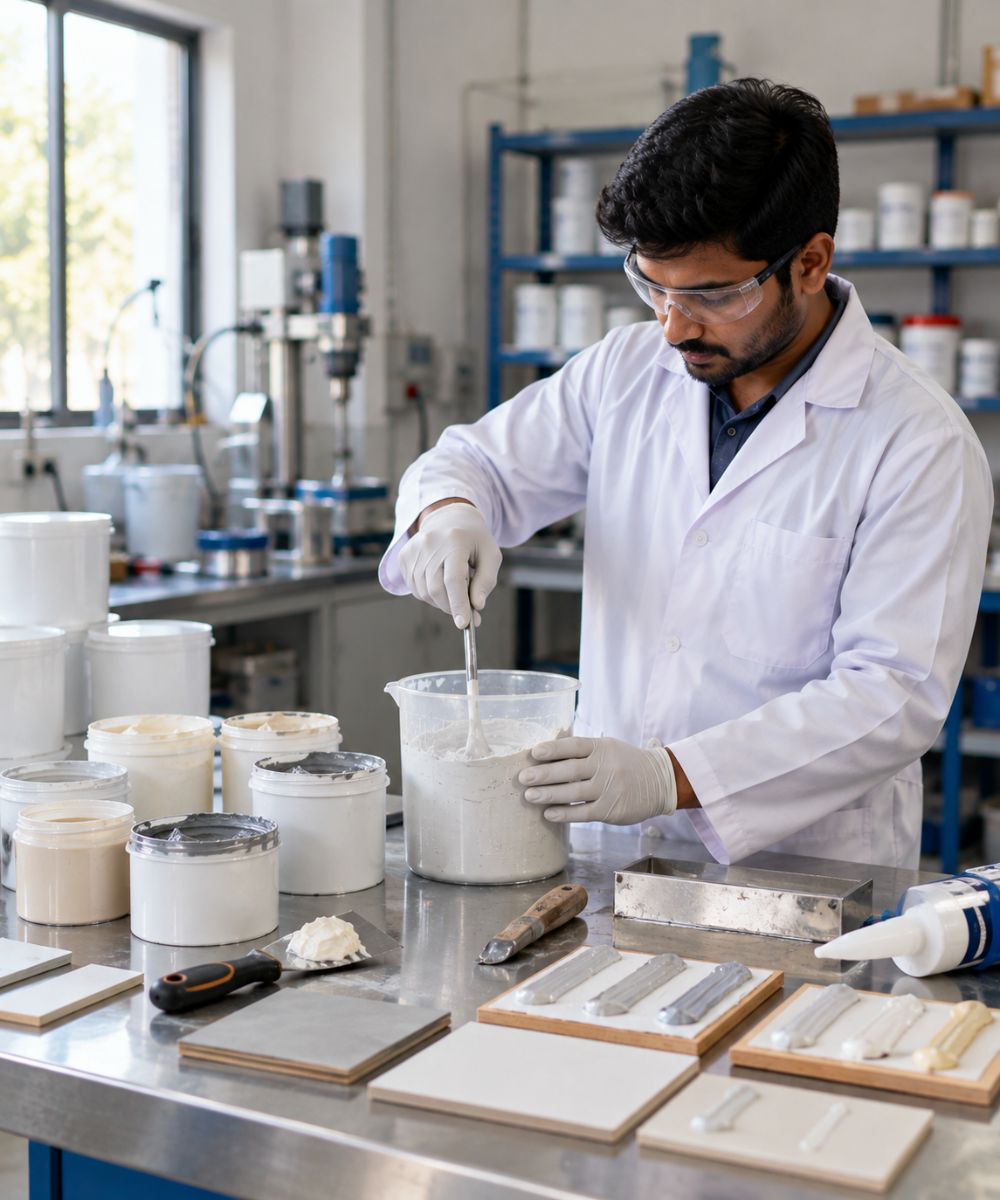
Solvent and chemical applications for relevant adhesive and sealant formulations.
Industrial Formulations
Industrial chemical and solvent applications for processing and manufacturing environments.
Process Industries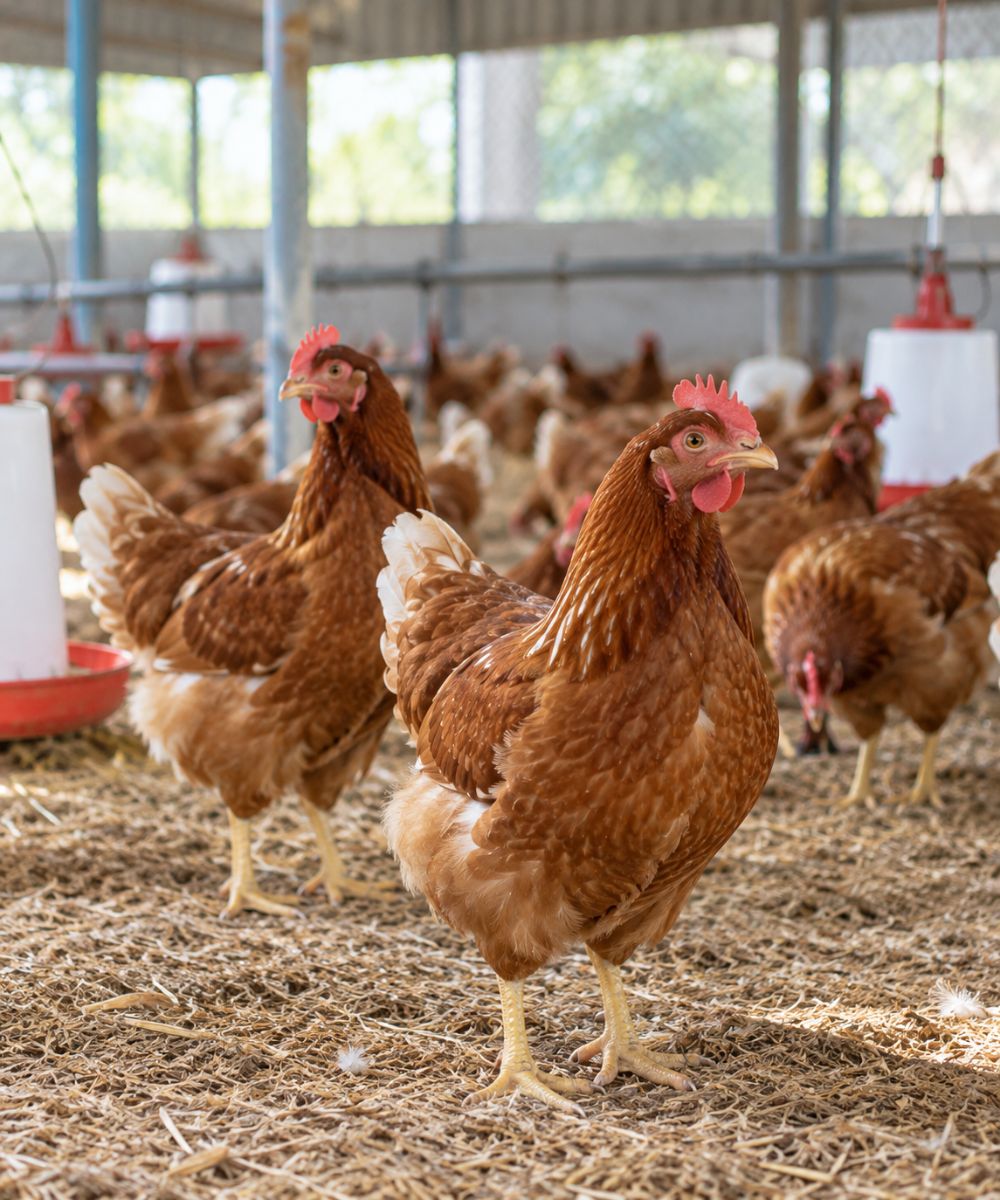
DDGS applications for animal feed sectors, including poultry and livestock nutrition.
Feed Applications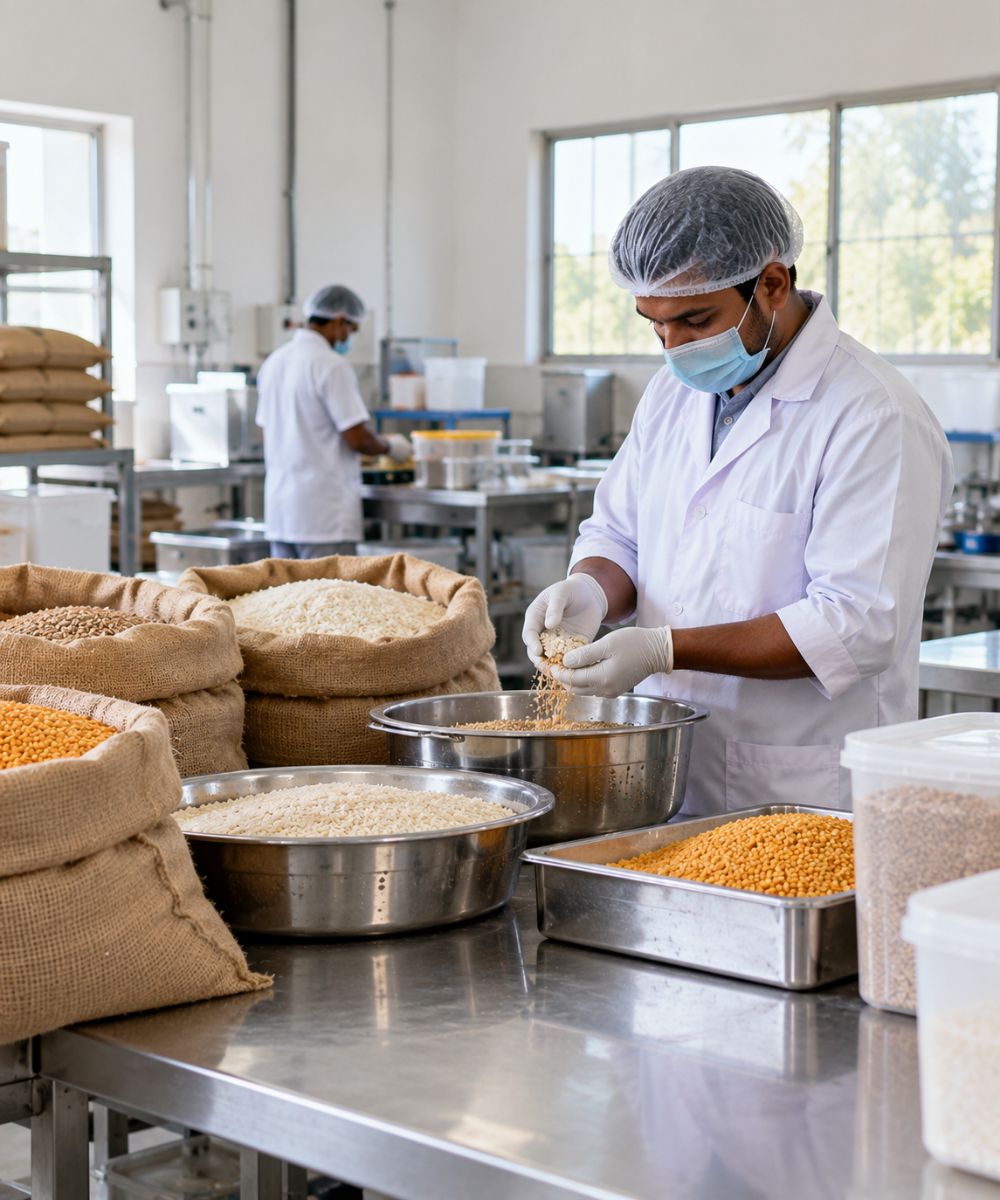
Chemical and process solutions for relevant food-processing applications.
Processing Applications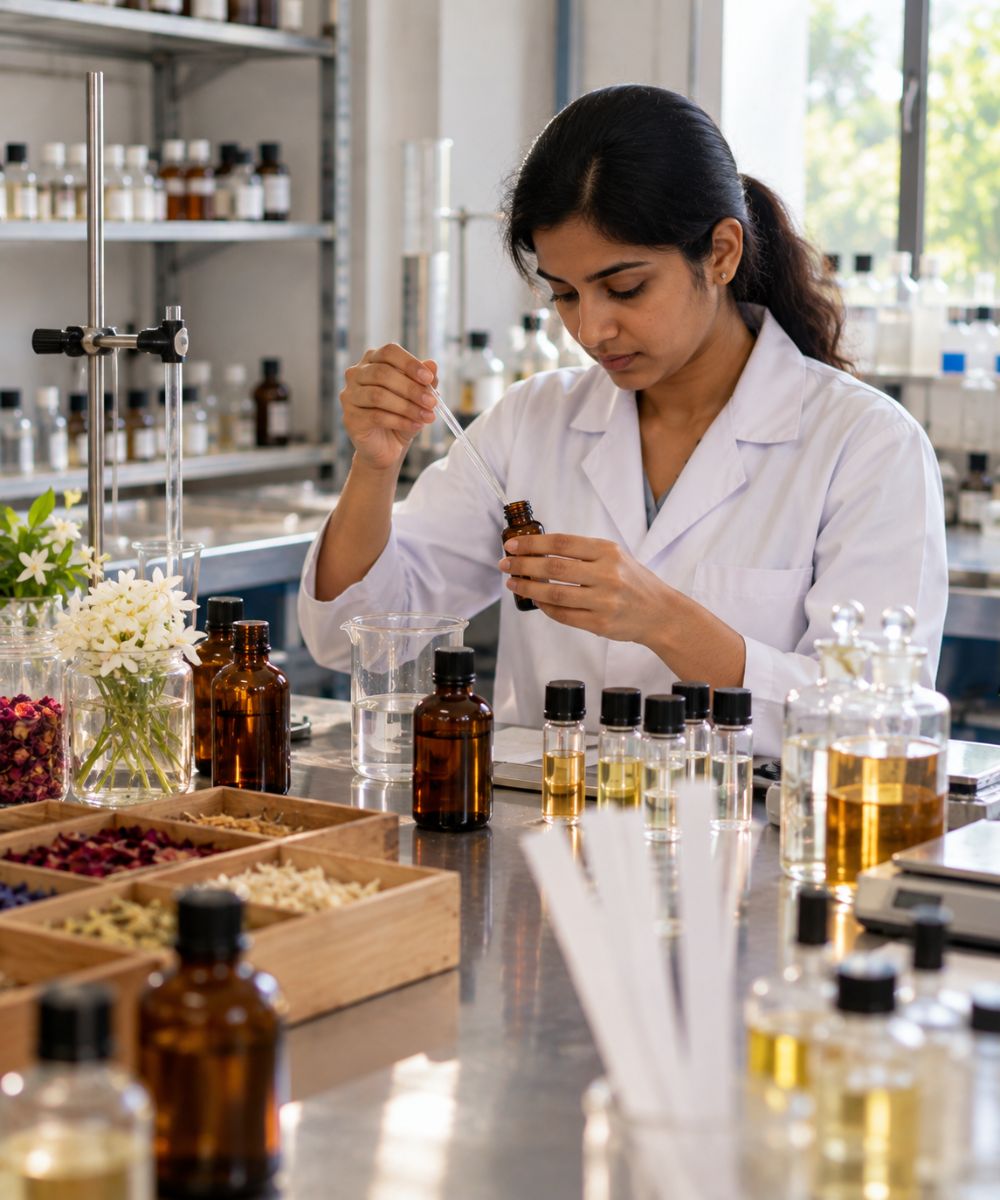
Solvent and chemical applications for relevant specialty formulations.
Specialty Applications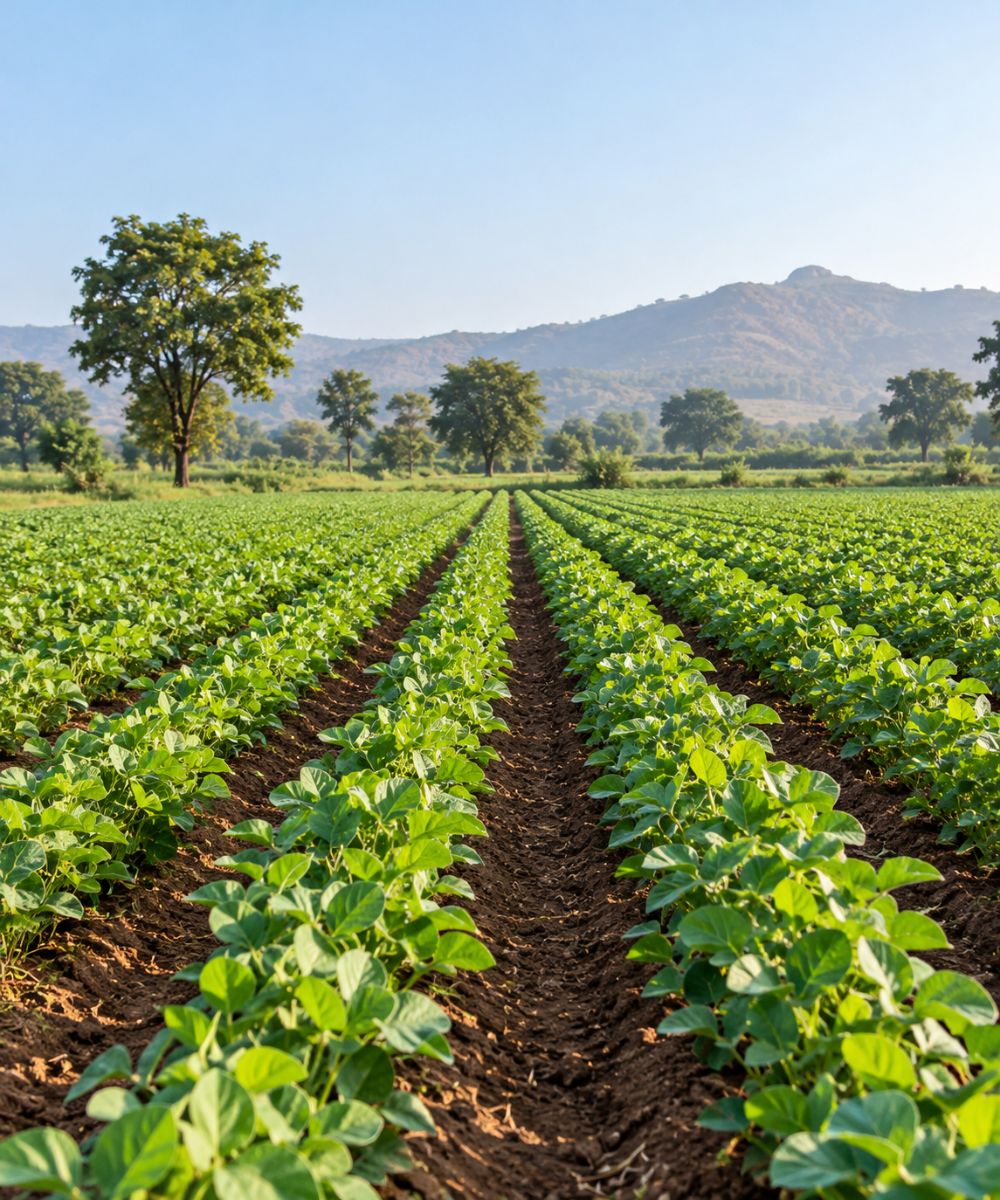
Bio-based products and agricultural co-products for relevant allied applications.
Agricultural Applications